


Welcome To Shawpak Systems Ltd
Established in 1984 Shawpak Systems prides itself on providing high level technical sales and support to our valued customer base. Offering solutions for Product Inspection, Packaging and Hygiene equipment sales and after sales support including certified customer training on site or at our Centre of Excellence training and demonstration facility.
What Our Clients Are Saying
North American Distributor Hygiene Equipment Solutions
Shawpak are the exclusive distributor in North America for Hygiene Solutions with complete parts and service support.
Product Safety
Our experience in the product inspection industry is essential to the success of our quality assurance program, because we can enhance the safety of your products by detecting contaminants, for the removal, before those products reach your consumers.
Protection and Trust
Protecting your customers, shareholders and brand is your ultimate goal. Ensuring that you have the proper equipment to do the job is ours.
Technical Advisors
Shawpak Systems Technical Advisors will guide you through the best practice options available based on your specific application, acting as your Trusted Advisor.

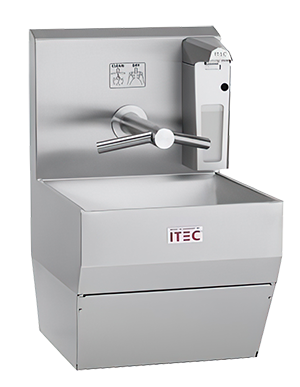
Food Plant Wash Basin
A food plant wash basin is a specialized hygiene station designed to meet sanitation requirements in food processing environments, where worker cleanliness directly affects product safety and regulatory compliance.
At a mid-sized meat processing facility near Oakville, Ontario, the plant manager faced a familiar pressure. Health inspections were becoming stricter. Line workers moved between different work zones throughout the shift, and the existing handwashing stations were neither positioned nor equipped to handle the volume or the specific contamination risks the operation faced. Supervisors reported bottlenecks during shift changes. More concerning, the facility's hygiene protocol relied on equipment that was difficult to maintain and inconsistent in performance.
The real cost was invisible until an audit flagged it: inadequate transition hygiene between raw material handling and finished product zones. The facility needed a solution that was not just compliant, but integrated into actual workflow. They needed to understand what equipment would actually work for their specific operation, not generic recommendations from a catalog.
Understanding the Facility's Workflow and Hygiene Gaps
Shawpak Systems Ltd began not with a sales pitch, but with an on-site assessment. The team spent time observing the plant's actual movement patterns, material flows, and the points where contamination risk was highest. This is where most equipment suppliers stop listening-Shawpak's approach is to understand the operation first.
The facility's primary need was clear: multiple strategically positioned wash stations that could handle high-frequency use without becoming a compliance liability. But the secondary need was equally important-the equipment had to be durable enough to withstand daily chemical cleaning, food-grade sanitation protocols, and constant moisture exposure. Stainless steel construction was essential. Ease of maintenance mattered as much as hygiene effectiveness.
Shawpak brought their technical advisory expertise to bear. They evaluated:
- Basin depth and width suitable for the glove and sleeve coverage the work required
- Water temperature and pressure consistency across multiple stations
- Drainage and sanitation protocols that would integrate with existing facility systems
- Complementary equipment-foot drying and industrial boot cleaner access points at the same stations
The facility also invested in a boot cleaning station positioned at the entrance to the raw materials zone. Because worker hygiene is a system, not isolated tasks, Shawpak recommended combining the wash basin installation with an industrial boot cleaner to prevent cross-contamination from the outside environment.
Selecting and Installing the Right Food Plant Wash Basin Solution
Equipment selection is where Shawpak's exclusive North American distribution relationship with Hygiene Solutions became the deciding factor. The facility gained access to commercial-grade systems designed specifically for food processing environments, not adapted from general industrial use.
The comparison below shows how this facility's solution stacked up against their original setup:
| Feature | Previous Setup | Shawpak Solution |
|---|---|---|
| Basin Material | Powder-coated steel | Food-grade stainless steel |
| Water Temperature Control | Manual valve adjustment | Thermostat-regulated consistency |
| Maintenance Frequency | Weekly deep cleaning + corrosion issues | Daily sanitization, no degradation |
| Drainage Standard | Manual trap cleaning | Hygiene-certified design, minimal blockage |
| Integrated Hygiene Flow | Separate, disconnected stations | Boot cleaner, basin, drying coordinated |
Installation took place over a single weekend to minimize production disruption. Shawpak's team handled placement, plumbing integration, and electrical connections for heated systems. More importantly, they provided on-site training to facility staff on proper operation, daily sanitization schedules, and troubleshooting. This is where many installations end; Shawpak stays involved through certified after-sales support across Canada and the USA, meaning replacement parts and technical guidance are available when needed.
The facility also integrated a shoe sanitizing station in the same area, creating a complete hygiene checkpoint rather than scattered equipment.
Within two weeks, the facility's next health inspection reflected the change. Inspectors noted the improvement in hygiene infrastructure. More measurable: line supervisors reported that the new stations reduced bottlenecks. Workers could move through hygiene protocols faster because the equipment was reliable and ergonomic. The facility's own audit data showed reduced microbial detection rates in the transition zones that had previously been flagged.
The installation also proved easier to scale. When the facility later expanded a second processing line, adding another wash basin and boot cleaning machine took weeks rather than months, because Shawpak already understood the operation and had the expertise to integrate new equipment into existing systems.
If your facility in Oakville or elsewhere across North America is managing similar hygiene challenges, the solution begins with understanding your actual workflow, not assuming standard equipment will suffice. Shawpak Systems Ltd brings the technical expertise to assess your operation, the access to purpose-built equipment through their exclusive distribution partnership, and the on-site training and support to make the installation meaningful. Reach out to discuss how a properly designed hygiene solution can improve both compliance and operational efficiency.
Frequently Asked Questions
What makes a food plant wash basin different from a standard sink?
A food plant wash basin is engineered for high-frequency industrial use with food safety compliance built in. It uses food-grade stainless steel to resist corrosion from sanitizing chemicals, includes thermostat-regulated water temperature for consistent hygiene protocols, and features drainage systems designed to prevent microbial accumulation. Standard sinks lack these specifications and degrade quickly under food processing sanitation demands.
Are there food plant wash basin suppliers near Oakville?
Shawpak Systems Ltd, based in Oakville, Ontario, is an established distributor and installer of food plant hygiene equipment serving North America since 1984. They provide not only equipment supply but also on-site technical assessment, installation, training, and certified after-sales support-services that extend across Canada and the USA.
How long does it take to install new wash basins in an operating facility?
Installation timing depends on the scope, but a single station can typically be completed in one to two days with minimal production disruption. Shawpak coordinates with your facility to schedule around production needs. More importantly, they provide on-site training immediately after installation so your team can operate and maintain the equipment correctly from day one.

Products to Suit Your Needs
- Hygiene Equipment
- Product Inspection
- Packaging Equipment
- Training and Demo Facility
- Sealing Equipment
- Custom Conveyors
- Consultant Service
- Direct Drive Technology
- Spare Parts
- Test Samples
Contact US
For general information or to set up an appointment please complete the form below or give us a call.
GENERAL INQUIRIES
Sales (905) 847 0122 EXT 1
Accounting (905) 847 0122 EXT 4